Explore the actual 3D model
Switch construction routes or separate the parts to see how they fit. Drag to rotate; use + / − to zoom, arrow keys to rotate, and Home to reset.
Loading the project model. The CAD preview remains available if 3D cannot start.
A shop support with a recognizable outline
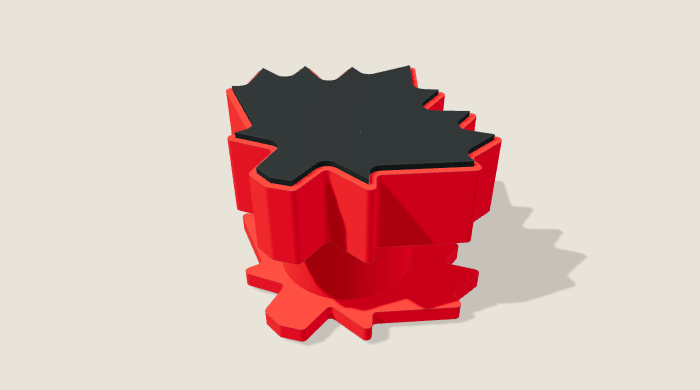
This project starts with a familiar workshop need: creating space beneath a board while keeping the contact surfaces clear of exposed metal. The maple outline carries the Dominant Goose identity into a practical bench accessory. In this revision, the upper body and lower foot share the same broad silhouette; separate rubber sheets provide the contact surfaces. The shape, pads and hardware are all visible in the actual model rather than a product illustration.
The intended set contains four supports. Each uses the same parts and can be assembled at either of two heights. This feature follows the existing DG-MAPLE-01 design and fabrication records at revision 0.2.2. It is a look inside an original project already developed here, with its physical prototype work still ahead.
Where the two heights come from
The low stack is straightforward: a 28 mm body sits on a 6 mm foot, with a 2 mm pad above and another below. That adds up to 38 mm. Insert the single 30 mm lift spacer between body and foot and the nominal padded height becomes 68 mm. Both figures include adhesive within the stated pad thickness; adding adhesive outside that allowance changes the result.
The rigid body and foot each occupy approximately 97.7 × 91.7 mm in plan. The spacer is a 50 mm diameter cylinder. These are dimensions of the designed parts, not a load rating or evidence that a tall assembly will resist tipping. The design uses one lift stage only. Making a taller tower by stacking extra spacers would depart from this revision.
The dowels locate; the bolt holds the stack together
Exploding the model reveals the useful part of the mechanism. Two steel dowels locate each mating joint. A central M6 through-bolt secures the complete stack, with its head recessed into the bottom foot and its nut recessed into the top body. Low mode uses two dowels and an M6 × 30 mm bolt. Lifted mode uses four dowels and an M6 × 60 mm bolt. The nut is reused.
Rubber and adhesive are not the lift connection. The two closed grip pads cover the hardware pockets after assembly. Accessing the fasteners therefore means peeling and replacing or rebonding the pads. That is a service tradeoff worth seeing before building: clean contact faces, but no instant height change. This revision uses 10.5 mm across-flats pockets; it does not use the older Maple Bench Cookie's 11.4 mm measured-bolt pocket.
The same assembly in wood or printed polymer
The wooden route uses a dry hardwood body, a flat plywood foot and a hardwood spacer. The existing actual-size patterns define the leaf contour, shared centre and locating holes, including which face each blind pocket starts from. Stock thickness and parallel faces matter as much as the outline. A nominal board or sheet thickness is not a substitute for measuring the finished parts.
The printed route uses the corresponding rigid meshes. PETG is the prototype material choice, with bought rubber or EPDM for the grip faces in either route. Its 3MF files contain geometry, not a proven printer profile. Open them in OrcaSlicer's normal GUI, select the actual printer and filament, and inspect the sliced layers. The displayed metal parts are inspection envelopes; they are not printable replacements for bought fasteners.
What the first prototype needs to settle
The source and exported models establish dimensions and assembly relationships. They cannot establish grip on a dusty bench, finish marking, adhesive retention or the behavior of a printed part under sustained load. No physical sample results are recorded for this revision. Build and inspect one assembly before committing to a set, then compare both height configurations under controlled conditions.
The current qualification plan proposes no rocking and no more than 0.25 mm total height spread across four supports. Those are targets to measure, not achieved specifications. Slip, tipping, deformation, creep and repeated fastener service also remain open. Until those results exist, this is a digital prototype to investigate, with no published working capacity or claim that it replaces a clamped workholding setup.
Materials & cut list
| Material | Quantity | Actual dimensions / specification |
|---|---|---|
| Wooden route: dry, straight-grained hardwood grip body | 1 for the first prototype; 4 for a complete set | Finished maple contour envelope approximately 97.7 × 91.7 × 28 mm. Allow extra stock for cutting; preserve actual 28 mm thickness. |
| Wooden route: flat plywood foot | 1 for the first prototype; 4 for a complete set | Matching maple contour, approximately 97.7 × 91.7 × 6 mm finished. Use actual 6 mm thickness and flat, parallel faces. |
| Wooden route: hardwood lift spacer | 1 per lifted support; omit in low mode | 50 mm diameter × 30 mm high, with flat, parallel end faces. |
| Printed route: PETG for the three rigid components | An alternative to the wooden body, foot and spacer; make 1 of each for a lifted prototype | Use the revision 0.2.2 body, foot and lift meshes at their original millimetre scale. Filament consumption is not yet measured. |
| Bought M6 hex bolts and matching M6 nut | 1 × 30 mm bolt, 1 × 60 mm bolt and 1 nut per support; only one bolt is installed at a time | 30 mm bolt for low mode; 60 mm for lifted mode. Verify actual head and nut fit in the 10.5 mm across-flats pockets and full nut engagement. |
| Steel locating dowels | 4 per lifted support; 2 used in low mode | 6 mm diameter × 10 mm long; nominal locating sockets are 6.3 mm diameter. Check actual fit before assembly. |
| Non-marking rubber or EPDM grip sheets | 2 pads per support; 8 for a complete set | Maple pad outline inset 2.2 mm from the rigid contour. Each pad is 2 mm total thickness including its adhesive; no centre holes. |
| Suitable removable pad adhesive | As required for the two contact pads | Include its film thickness within the 2 mm pad allowance. Check retention and compatibility with the chosen rubber and test finish. |
Tools
- Ruler, square, calipers, depth gauge and a flat reference surface
- Wooden route: suitable saw, files or abrasives, and tools for forming the dimensioned hex pockets
- Wooden route: drill press or appropriate guided drilling setup with depth control and 6.6 mm and 6.3 mm drills
- Clamps or a vise and a stable work surface for cutting and drilling
- Printed route: suitable FDM printer, filament and OrcaSlicer using its normal GUI
- Hand tools matching the purchased M6 bolt and nut, plus suitable tools for cutting the rubber pads
- Eye protection and appropriate dust control for fabrication
Before you start
- Secure stock for cutting and drilling. Never hold a small part freehand at a drill press; use suitable clamping and follow the machine and bit instructions. Wear eye protection.
- Use controlled drilling depths and verify them on scrap. Stop the machine before measuring, clearing chips or adjusting the work. Keep hands clear of cutting paths and rotating tools.
- Use appropriate extraction and respiratory protection for wood dust. Clean settled dust with a suitable HEPA-filtered vacuum or damp cloth; do not blow it into the air with compressed air.
- Keep prototype evaluation separate from routine workholding. Grip, tipping, load capacity, printed-layer behavior and long-term creep are unqualified; this design does not establish a safe powered-cutting setup.
- Use one lift spacer only. Reject cracked, warped or loose components, damaged pockets, slipping pads and any assembly with exposed metal at a contact face.
Prototype build sequence
Check the revision and actual hardware
Start with one assembly from DG-MAPLE-01 revision 0.2.2. Measure the purchased bolts, nut and dowels before making their mating parts. For a wooden prototype, use the existing patterns at Actual size and verify both the 50 mm horizontal check and 20 × 20 mm square before transferring anything. The material list describes one prototype first; multiply the appropriate quantities only after its checks pass.
Check: Confirm the selected construction route, actual stock thicknesses and purchased hardware dimensions. Stop if the pattern scale, hardware or stock does not match the design.
Make the rigid parts in the chosen route
For wood, use the existing maple body and foot patterns and the 50 mm spacer pattern. Keep the working faces flat and parallel and transfer the common centre and dowel datums before machining. For printing, use the existing bed-oriented body, foot and lift geometry at its original scale. Open it in OrcaSlicer's normal GUI and inspect layer continuity, downward holes, bridges and bed contact using the actual printer and material setup.
Check: Measure the 28 mm body, 6 mm foot and optional 30 mm spacer. Reject warped, cracked or damaged parts. A successful model export or slicer preview does not establish physical strength.
Inspect the pockets and locating sockets
The centre shaft bore is 6.6 mm. The body's upper nut pocket is 10.5 mm across flats and 6 mm deep; its two lower dowel sockets are 6.3 mm diameter × 6 mm deep. The foot's underside bolt-head pocket is 10.5 mm across flats × 4 mm deep; its upper dowel sockets are 5 mm deep, leaving 1 mm beneath them. Dowel centres are 16 mm either side of the central shaft. The spacer has a through shaft bore and two sockets per end: 6 mm deep from its bottom and 5 mm from its top. Use the stated face datums and controlled depths when machining wood; inspect the same features on printed parts.
Check: Measure every blind depth and test the actual hardware without force. Do not break through the foot's thin socket floors or conceal a fastener that stands proud.
Assemble the low configuration first
Seat two locating dowels in the foot and place the body directly on it. Insert the M6 × 30 mm bolt from below and seat the matching nut in the upper pocket. Tighten by hand with suitable tools, checking that the faces close flat and the nut fully engages. Leave the pads off while inspecting the concealed hardware positions.
Check: The joint should close without rocking, trapped debris or a dowel bottoming prematurely. Inspect the head, nut and threads; stop if the connection is loose or the pockets are damaged.
Check the single lift stage
Exchange the short bolt for the M6 × 60 mm bolt and place one 30 mm spacer between foot and body. Use two dowels at each joint, four in total. Confirm the spacer orientation so its different socket depths meet the intended parts. Recheck engagement and face contact before adding pads. Additional stacked spacers are outside this design.
Check: Both joints must close without force or rocking. Confirm that the longer bolt fully engages the nut and that all hardware remains inside its pockets.
Fit the replaceable grip pads
Cut the closed maple pad outlines from suitable rubber or EPDM. Fit one above and one below, keeping the total thickness of each pad and adhesive at 2 mm. Bond them only after the hardware checks pass. Test the selected adhesive and contact material on scrap. To change height later, peel the pads to expose the fasteners, then replace or rebond and inspect them again.
Check: Contact faces must be clean, smooth and free of exposed metal. Check pad retention and finish marking on scrap; the adhesive does not replace the bolt and dowel connection.
Record the prototype results before making four
Measure the assembled heights and check the prototype on a flat reference in both configurations. Record fabrication route, material, actual hardware, dimensions and observed failures. The existing qualification plan then calls for controlled grip, tipping, compression, creep and service checks before establishing a working limit. If making four, measure their total height spread in both configurations against the proposed 0.25 mm target.
Check: Do not treat successful assembly as a load or grip test. No physical results are currently recorded for revision 0.2.2; hold off on a full set if fit, flatness or retention is unresolved.
Check before use
- Confirm revision 0.2.2 and actual millimetre scale; do not substitute the older Cookie's 11.4 mm pocket for this design's 10.5 mm pockets.
- Cross-check nominal padded heights: 28 + 6 + 2 + 2 = 38 mm; adding the single 30 mm spacer gives 68 mm. Measure the physical result, including adhesive.
- Check the purchased bolt, nut and dowels against every bore and pocket. Verify full nut engagement, closed joints and recessed hardware in both height configurations.
- On a flat reference, check for rocking. For four supports, record the largest minus smallest assembled height in each configuration; 0.25 mm is a proposed maximum spread, not a measured result.
- Inspect pad retention, clean contact and finish compatibility on scrap. Grip, tipping, load, creep and repeated service need separate physical qualification before a working limit can be stated.
Safety references
These references cover working practices. They do not certify or validate this project design.